


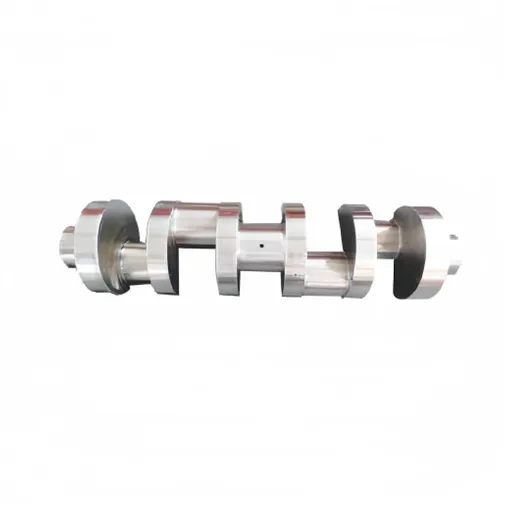
Cementing Pump Crankshaft Assembly
Cementing Pump Crankshaft Assembly
Heavy-duty power-end replacement assembly engineered for high-pressure triplex and quintuplex cementing pumps. Built for direct OEM interchangeability and structural endurance under cyclical high-load operating conditions.
Product Overview
The Cementing Pump Crankshaft Assembly serves as the mechanical heart of the power end, translating rotational torque from the transmission into linear plunger movement at the fluid end.
Manufactured from heavy-section alloy steel forgings, each assembly undergoes precision CNC machining, deep-hole drilling for lubrication channels, and induction hardening to withstand extreme shock loads and continuous cyclic fatigue in oilfield environments. Supplied as a balanced assembly (including crankshaft, main bearings, and gear mounting flanges where applicable), it drops directly into standard power-end housings.
Key Features
High Fatigue Resistance: Forged alloy steel grain flow optimized around crankthrows to prevent stress concentration and micro-cracking under cyclic loading.
Optimized Lubrication Channels: Internal cross-drilled oil galleries deliver pressurized lubrication directly to connecting rod journals, reducing friction and bearing wear at high RPM.
Surface Hardened Journals: Main and crank journals induction-hardened to HRC 55–60, ensuring high wear resistance while maintaining a tough, ductile core.
Dynamic Balancing: Dynamically balanced on high-precision rigs to minimize vibration, bearing wear, and power-end housing fatigue during high-speed operation.
Technical Specifications
|
Parameter |
Specification Range / Standard |
|
Compatible Pump Types |
Triplex / Quintuplex Cementing Pumps (Standard OEM equivalents) |
|
Material Grade |
4340 Alloy Steel / 20CrMnMo (Customizable per load specs) |
|
Forging Ratio |
≥ 4:1 (Closed-die or open-die heavy forging) |
|
Journal Hardness |
HRC 55–60 (Depth: 3.0–5.0 mm) |
|
Dimensional Tolerance |
Ground to ISO tolerance class IT6–IT7 |
|
Non-Destructive Testing |
100% Ultrasonic (UT) and Magnetic Particle (MT) inspected |
|
Weight Range |
300 kg - 1,200 kg (Model dependent) |
Applications
Primary & Remedial Cementing
Integrated into skid-mounted or truck-mounted cementing units handling slurry injection up to 15,000 psi.
Rig Equipment Overhaul
Standard replacement assembly for routine maintenance and rebuilding of field-worn power ends.
Auxiliary Pumping Services
Compatible with heavy-duty mud circulation, acidizing, and pressure testing spreads.
Materials & Configuration
Material Selection
Forged 4340 / 34CrNiMo6: High tensile and yield strength suited for high-torque oilfield applications.
Metallurgical Control: Vacuum degassed steel to eliminate internal inclusions, verified via spectrometer analysis per heat lot.
Configuration Options
Crankshaft Type: Single-piece integral forging (standard for triplex units).
Included Components: Supplied bare or pre-fitted with timing gears, bearing inner races, and oil seals based on assembly requirements.
Manufacturing & Quality Control
Production relies on heavy industrial manufacturing processes backed by strict quality verification at every critical stage:
Forging & Thermal Processing: Controlled closed-die forging followed by normalizing, quenching, and tempering to achieve uniform microstructures.
Precision Machining: CNC heavy-duty lathes and dedicated crankshaft grinding machines maintain journal roundness within 0.01 mm.
Mandatory Inspection Protocols:
Ultrasonic Testing (UT): Detects internal porosities, inclusions, or forging flaws.
Magnetic Particle Testing (MT): Surface and subsurface crack detection on all critical fillet radii.
Hardness Testing: Rockwell/Brinell hardness verification across journals and shaft ends.
Dimensional CMM Inspection: Full coordinate measurement report provided with each unit.
Verification Media Note: To verify internal integrity and dimensional precision prior to site deployment, mill test reports and inspection footage (including UT/MT testing procedures and dynamic balancing logs) are available for review per production batch.
Customization & OEM Integration
Model Matching
Reverse engineering and production based on OEM part numbers, sample drawings, or physical worn units.
Dimensional Modification
Custom journal diameters, keyway locations, and spline configurations to fit non-standard power-end conversions.
Documentation Support
Material Test Reports (MTRs to EN 10204 3.1), balancing certificates, and inspection data packages supplied with shipment.
Packaging & Shipping
Export Packaging: Sealed in VCI (Volatile Corrosion Inhibitor) anti-rust bags, secured in heavy-duty fumigated wooden crates with internal bracing to prevent shift during transit.
Lifting Provisions: Crates equipped with forklift pockets and designated crane lifting points for safe rigging.
Logistics: Flexible FOB/CIF shipping via ocean freight or air cargo from major industrial ports.
Frequently Asked Questions
Q: Are these crankshaft assemblies interchangeable with original OEM power ends?
A: Yes. Machining tolerances and critical dimensions (stroke, journal diameters, center-to-center distances) match standard oilfield cementing pump configurations to allow direct drop-in replacement without housing modification.
Q: What material certifications are provided with the crankshaft?
A: Each unit ships with a full Material Test Report (MTR) conforming to EN 10204 3.1, detailing chemical composition, mechanical properties, and heat treatment logs.
Q: Is balancing performed before shipment?
A: Yes. Every crankshaft is dynamically balanced on high-precision balancing machines. Residual unbalance is corrected within strict ISO standards to minimize vibration during operation.
Q: Can you manufacture custom crankshafts from provided drawings?
A: Yes. We accept custom orders based on engineering drawings, 3D models, or precise physical sample measurements, with typical production lead times confirmed during technical review.
Q: What non-destructive testing (NDT) is performed?
A: 100% of our crankshaft forgings undergo Ultrasonic Testing (UT) for internal soundness and Magnetic Particle Testing (MT) for surface defect verification prior to final shipment.
Q: What is the recommended maintenance practice for extending crankshaft service life?
A: Ensure clean, filtered lubrication oil is supplied continuously to the power end, monitor operating oil temperature, and inspect bearing clearances and fillet radii during scheduled rig overhauls.
Request a Quote
To generate an accurate quotation and technical review, please provide the following details in your inquiry:
Pump Model & OEM Part Number (e.g., SPM TWS 600, Halliburton HT-400, or custom spec).
Required Quantity.
Target Delivery Terms (FOB, CIF, EXW) and destination port.
Technical Attachments (Drawings, specifications, or material preference if non-standard).
Expected Delivery Timeline.
Hot Tags: cementing pump crankshaft assembly, China cementing pump crankshaft assembly suppliers, factory
Previous
No InformationNext
No InformationYou Might Also Like
Send Inquiry